Gripper Conveyors for Bottle Handling
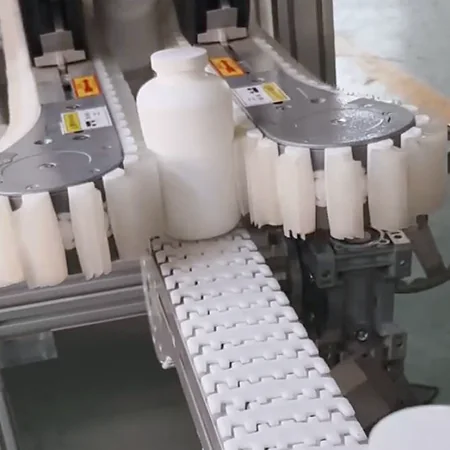
A gripper conveyor uses opposing side-contact surfaces to control a product as it moves. Our bottle gripper conveyor uses this side-grip arrangement to transfer bottles between conveyors. The bottle profile and available contact area determine where it can be gripped.
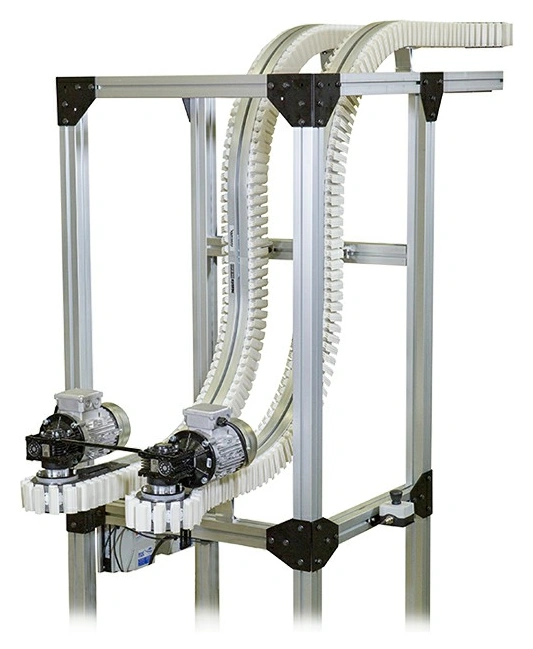
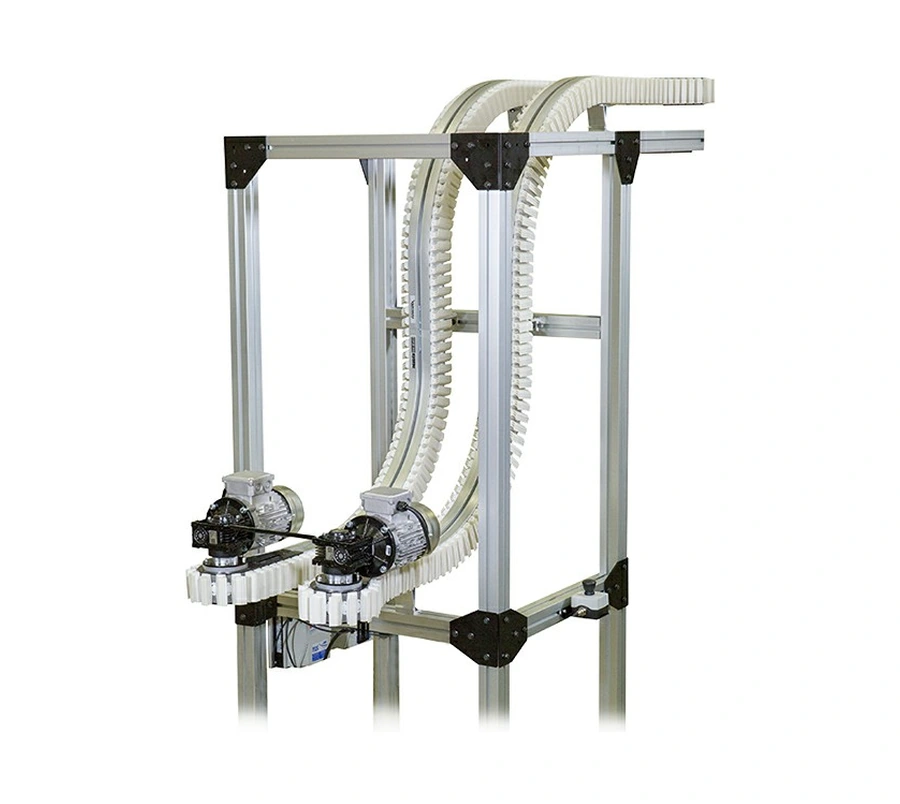
CSTRANS Bottle Gripper Conveyor
Our gripper conveyor for bottles is selected around the bottle and the transfer between the connecting conveyors. Photos of the bottle and the line help us consider both parts of the application together.
| Parameter | Specification or Option |
|---|---|
| Conveying Speed | Adjustable, 1–60 m/min |
| Conveyor Height | Adjustable, 200–1000 mm |
| Voltage | 220 / 380 / 415 V |
Side-Grip Support Through the Transfer
The moving contact surfaces engage opposite sides of the bottle and carry it through the gripping section. Where the bottle leaves the supporting surface of the infeed conveyor, the side grip must take over its support. At discharge, the receiving conveyor must support the bottle as it leaves the grip. The contact length and the position of both transfers therefore form part of the handling arrangement.
Grip spacing and contact material affect both the holding force and the pressure on the bottle walls. A filled bottle increases the load carried through the contact area; a flexible empty bottle may respond differently to the same grip setting. Bottle material, shape and operating weight are considered together when selecting the gripping arrangement.
Bottle Profile and Grip Area
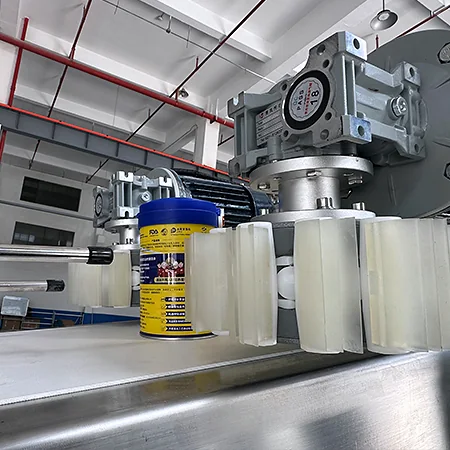
The usable grip area changes with the bottle profile and the position of labels or sleeves. Bottles with similar overall dimensions can have different contact surfaces. The gripping arrangement therefore depends on the usable contact area as well as the outline.
Front and side views with dimensions show the area available for side contact. Marking labels, sleeves and other surfaces that need particular care helps identify the limits of that area.
Empty and filled bottles place different loads on the gripping arrangement. Selection needs to account for the operating condition and weight. Where the line handles several bottle sizes, the smallest and largest examples establish the range the proposed configuration must accommodate.
Infeed and Discharge Requirements
The transfer is defined by the infeed and discharge heights, bottle orientation at each end and direction of travel. The target handling rate and gap between bottles are also needed to assess the arrangement.
The layout shows any elevation change, required reorientation or process access, together with where the bottle starts and how it must arrive at the next machine.
Request a Bottle Gripper Conveyor Quote
For a quote, send bottle photos and dimensions, empty or filled weights, and a line layout. Include the available grip area and the required transfer at each end.